Thickness consistency is one of the key quality indicators in SPC flooring production. When the flooring core sheet is too thick in some areas and too thin in others, manufacturers may face problems during lamination, cutting, profiling, and final product inspection. Even when the average thickness meets the specification, local variations can still affect finished flooring quality.
To improve thickness consistency in SPC flooring production, manufacturers need to control the entire process rather than adjust only one machine setting. Material formulation, feeding stability, extrusion pressure, calendering conditions, cooling, and haul-off speed can all influence the final sheet thickness.
For manufacturers evaluating a new SPC flooring extrusion line, these factors should be considered together because stable output depends on how the complete production system works as a unit.
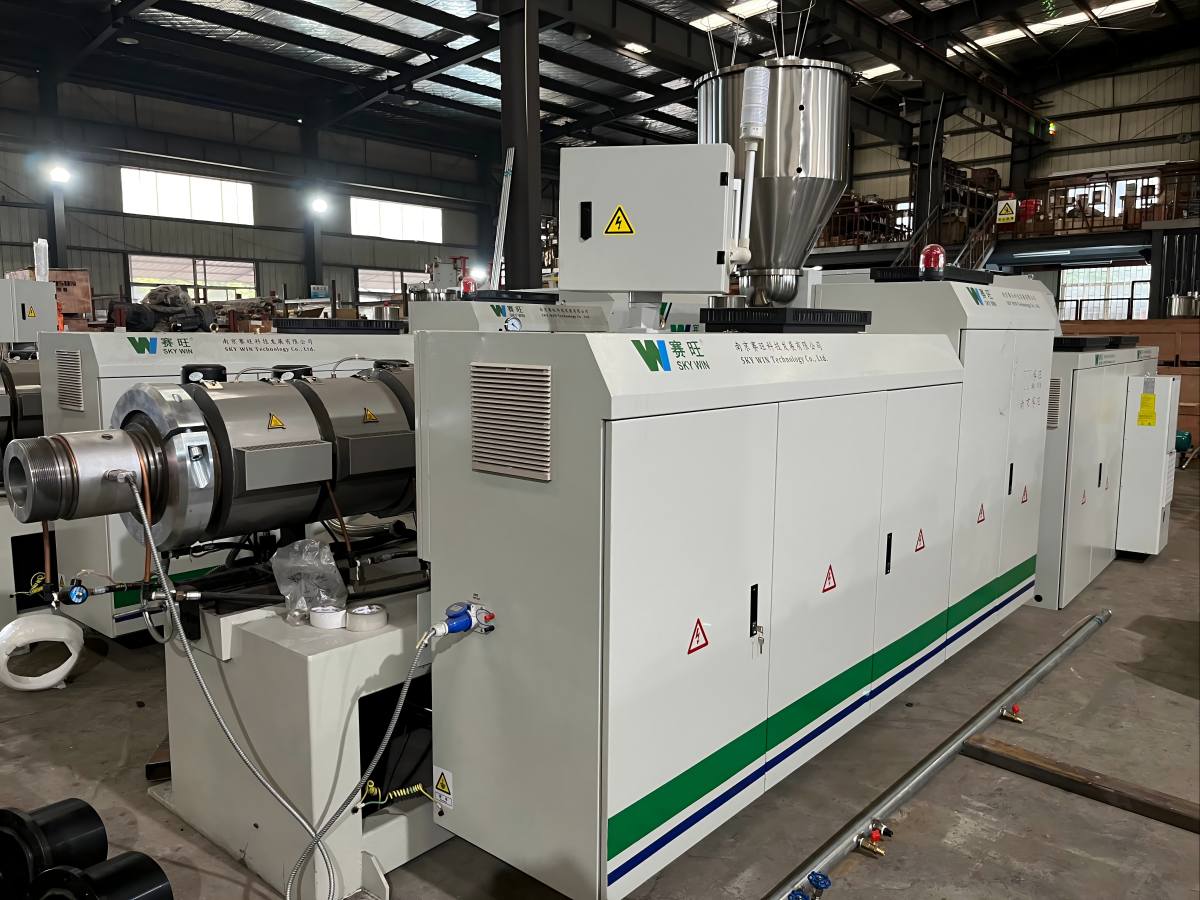
SPC flooring sheet production equipment used to process PVC and calcium carbonate composite materials.
What Causes Thickness Variation in SPC Flooring?
Thickness variation usually results from several process conditions interacting with each other. Before changing machine settings, operators should identify whether the problem is related to material feeding, extrusion, the calendering section, cooling, or downstream pulling.
Common causes include:
- Unstable material feeding: Fluctuations in the amount of compound entering the extruder can cause variations in output and sheet thickness.
- Inconsistent melt temperature: Changes in material plasticization and melt flow can affect how evenly the compound spreads across the sheet width.
- Uneven calender roll conditions: Roll gap, alignment, surface condition, and temperature differences can contribute to thickness variation.
- Unstable haul-off speed: Excessive or fluctuating pulling force can stretch the sheet and change its measured thickness.
- Uneven cooling: Differences in cooling conditions may cause dimensional changes or residual stress that affects later measurements.
- Inconsistent raw materials: Changes in PVC resin, calcium carbonate, stabilizers, or lubricant proportions can affect processing behavior.
A useful first step is to record where the variation occurs. If thickness changes over time at the same measuring point, investigate process stability. If the center is consistently thicker than the edges, inspect the calendering system and material distribution across the sheet width.
Keep Raw Material Feeding and Formulation Consistent
Stable sheet thickness starts before the compound enters the extruder. SPC flooring commonly uses PVC resin, calcium carbonate, stabilizers, and processing additives. Differences in batch composition, mixing quality, bulk density, or feeding rate can change the way the material melts and flows.
Manufacturers should use a controlled formulation and follow the same material preparation procedure for each production batch. Check weighing equipment, feeder calibration, mixing time, and material handling practices. If recycled material is used, its proportion and processing characteristics should also be controlled.
When a thickness problem appears after changing suppliers or switching material batches, compare the affected batch with a previously stable batch before making major machine adjustments. This helps prevent operators from compensating for a material issue by introducing unnecessary changes to the extrusion process.
It is also important to maintain a consistent feeding rate. Surges or interruptions in feeding can lead to output fluctuations, making it difficult for the downstream calendering system to maintain a stable sheet profile.
Stabilize Extrusion Temperature and Output
The extruder must plasticize the compound consistently and deliver a stable melt flow to the downstream equipment. If temperature distribution, screw operation, or material feeding changes significantly during production, the sheet may develop thickness fluctuations even when the calender roll gap remains unchanged.
Operators should monitor the following conditions:
- Temperature readings across the extruder zones and die.
- Main motor load and signs of unstable extrusion pressure.
- Material feeding rate and consistency between batches.
- Output changes during startup, speed adjustments, and continuous production.
- Abnormal wear, buildup, or restrictions around the screw, die, and melt-flow path.
Do not assume that increasing temperature or screw speed will automatically improve thickness consistency. Excessive changes can affect material viscosity, plasticization, and production stability. Adjust settings in a controlled manner and allow the process to stabilize before measuring the result.
For equipment selection, the extruder should be matched to the formulation, target sheet width, required thickness range, and planned output. SKY WIN's SPC/LVT/WPC flooring extrusion machines category provides a starting point for comparing equipment intended for different flooring production requirements.
Control Calender Roll Gap and Roll Temperature
Calendering is one of the most important stages for controlling the thickness of an SPC flooring base sheet. The roll gap influences sheet thickness, while roll alignment, temperature uniformity, and pressure distribution affect how evenly the material passes through the rolls.
If the sheet is consistently thicker in the middle and thinner at the edges, or the reverse, checking the calendering section should be a priority. Possible causes include uneven roll temperature, roll deflection under load, incorrect alignment, uneven material distribution, or a gap that is not set consistently across the working width.
To improve control:
- Check roll alignment and inspect the roll surfaces for wear or material buildup.
- Verify the roll gap at several positions across the working width, following the equipment manufacturer's procedure.
- Monitor roll temperature stability instead of relying on a single temperature reading.
- Make small, documented adjustments and measure the effect before making further changes.
- Keep the same measurement locations when comparing samples before and after an adjustment.
Calender roll gap should not be treated as a direct substitute for final thickness measurement. The sheet may change dimension as it leaves the rolls and cools, so measurements should be taken at a defined point in the process and checked again after the sheet reaches a stable condition.
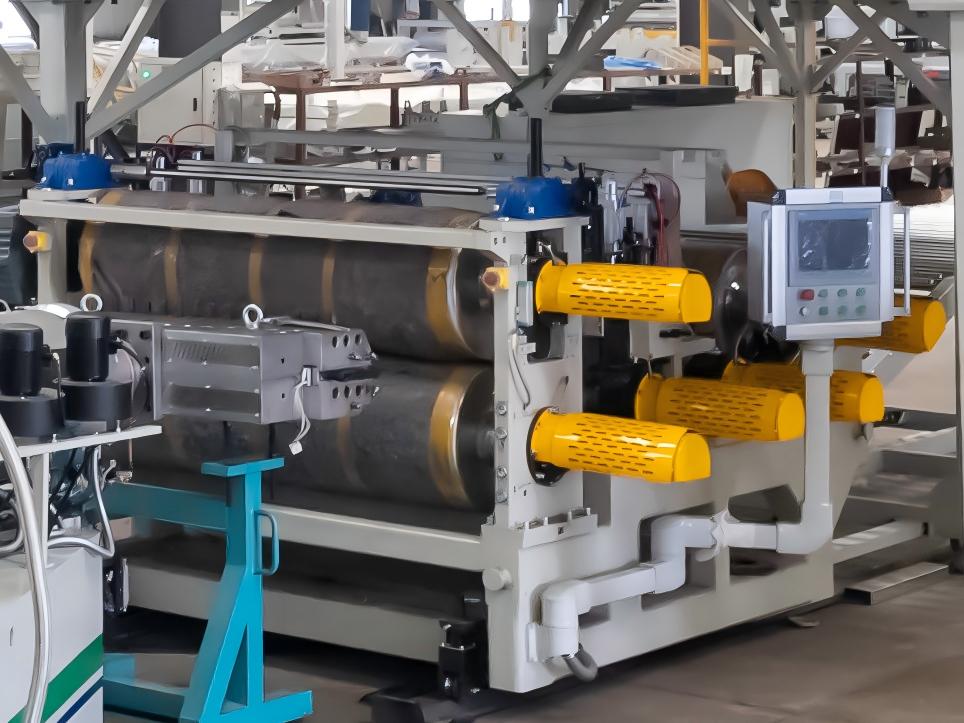
The calendering section plays an important role in controlling sheet thickness and material distribution.
Match Haul-Off Speed with Extrusion Output
The haul-off unit pulls the sheet through the downstream section. If pulling speed is not coordinated with extrusion output and calendering conditions, the sheet may be stretched or subjected to unstable tension.
When the sheet becomes thinner as the line speed increases, check whether the haul-off speed is rising faster than the extrusion output can support. If the sheet thickness fluctuates during speed changes, inspect the synchronization between the extruder, calender, haul-off unit, and cutting system.
Practical checks include:
- Confirm that the line speed remains stable during normal production.
- Check whether the sheet is being pulled excessively or accumulating material before the haul-off.
- Observe whether thickness changes coincide with speed adjustments.
- Verify that the drive and control systems maintain coordinated operation between production sections.
Operators should establish a stable baseline before increasing output. After a speed change, allow the line to settle and measure the sheet again rather than assuming the previous settings will deliver the same thickness at the new production rate.
Make Cooling More Uniform
Cooling affects dimensional stability after the sheet passes through the calendering section. If cooling is uneven across the sheet width or through the material, the sheet may retain residual stress or change dimension as it cools.
Check whether cooling conditions are consistent across the working width. Inspect the cooling system, water flow where applicable, roll temperatures, and the condition of cooling components. The correct setup depends on the line design, material formulation, sheet thickness, and production speed.
It is important to distinguish between a thickness variation created during calendering and a dimensional change that develops during cooling. Measure the sheet at a consistent location immediately after forming and again after cooling. If the initial thickness profile is already uneven, investigate extrusion and calendering first. If the profile changes significantly after cooling, review cooling uniformity and residual stress.
An integrated extrusion line needs coordinated forming, cooling, and downstream handling to maintain stable sheet quality.
Measure Thickness Across the Sheet Width
A single measurement cannot show whether an SPC sheet has a consistent thickness profile. Measurements should cover both the machine direction and the transverse direction so operators can identify whether the variation is continuous, localized, or related to changes in line speed.
A practical quality-control routine includes:
- Measure several positions across the sheet width, including the center and both sides.
- Take repeated samples at defined time intervals during stable production.
- Record the line speed, material batch, temperature settings, and relevant machine adjustments.
- Compare measurements taken before and after cooling when diagnosing dimensional changes.
- Use calibrated measuring equipment and the same measurement method for each sample.
The target thickness and allowable tolerance should come from the customer's product specification. Do not use one universal tolerance for every SPC flooring product, because the required limits depend on the product design, nominal thickness, and downstream processing requirements.
SKY WIN's published SWDB5 series specifications list sheet thickness options from 1.5 to 7 mm and sheet widths from 970 to 1220 mm across the listed configurations. These are equipment specifications, not a guarantee of thickness tolerance. Actual consistency depends on the selected configuration, formulation, operating conditions, and quality-control procedure.
Choose an SPC Flooring Line for Stable Production
When thickness variation continues despite careful process adjustment, manufacturers should evaluate whether the production line is appropriately configured for the target product. Important considerations include extruder capacity, calender roll design, temperature control, cooling capacity, haul-off synchronization, and the control system connecting the individual sections.
For a new project, provide the equipment supplier with the target sheet thickness, working width, material formulation, planned output, and required tolerance. These details make it easier to assess whether the proposed line is suitable for the actual production requirements.
The PVC Flooring (SPC/LVT) Sheet Extrusion Line is one of SKY WIN's relevant equipment options for manufacturers producing SPC and LVT flooring sheets. Its published system configuration includes an extruder, five-roll laminator, laminating unit, oil-heated roll system, cooling support frame, cooling system, edge trimmer, haul-off unit, sheet cutter, and electrical control system.
Because thickness consistency depends on the complete process, the goal is not simply to select a higher-output extruder. The line must maintain a suitable balance between extrusion output, calendering, cooling, and sheet handling at the required production speed.
A Practical Troubleshooting Checklist
When SPC flooring sheet thickness falls outside the target range, use a structured troubleshooting sequence rather than changing multiple parameters at once.
- Confirm the measurement: Check the measuring tool, sample location, and measurement method.
- Identify the pattern: Determine whether the variation occurs across the width, along the production direction, or after cooling.
- Review raw materials: Check the formulation, batch records, mixing, and feeding stability.
- Inspect extrusion conditions: Review temperature readings, motor load, output stability, and die condition.
- Check calendering: Inspect roll alignment, roll gap, roll temperature, and material distribution.
- Verify line synchronization: Compare extrusion output with calender and haul-off speeds.
- Review cooling: Check whether the sheet profile changes between forming and the final measurement point.
- Record the result: Change one parameter at a time and document the effect before continuing.
This approach helps operators isolate the source of variation, reduce unnecessary adjustments, and establish a repeatable production process. For manufacturers, repeatability is just as important as achieving the target thickness in a single sample.
Frequently Asked Questions
How can manufacturers improve thickness consistency in SPC flooring production?
Manufacturers should stabilize raw material feeding and extrusion output, control calender roll gap and temperature, synchronize haul-off speed, maintain uniform cooling, and measure thickness at consistent locations. The most effective adjustment depends on where the variation begins.
Why is SPC flooring sheet thicker in the center than at the edges?
A center-to-edge thickness difference may be caused by uneven material distribution, calender roll alignment or deflection, non-uniform roll temperature, or an inconsistent roll gap. Measure the sheet across its width and inspect the calendering section before changing unrelated settings.
Can extrusion temperature affect SPC flooring thickness?
Yes. Temperature influences material plasticization and melt flow. Unstable temperature conditions can contribute to output variation and uneven material distribution. Temperature adjustments should be based on the material formulation and equipment manufacturer's operating guidance.
Does haul-off speed affect sheet thickness?
Yes. If the haul-off pulls faster than the extrusion and calendering sections can supply material, the sheet may stretch and become thinner. Check speed synchronization and observe thickness during controlled speed changes.
How should SPC flooring sheet thickness be measured?
Use calibrated measuring equipment and measure multiple positions across the width and along the production direction. Keep sample locations and measurement timing consistent, and compare results with the product's specified nominal thickness and allowable tolerance.
What sheet thickness can a SKY WIN SPC flooring extrusion line produce?
SKY WIN's published SWDB5 series specifications list sheet thicknesses from 1.5 to 7 mm and widths from 970 to 1220 mm across the listed configurations. The appropriate model depends on the required product dimensions, output, formulation, and production conditions.
Will a higher-output extrusion line automatically improve thickness consistency?
No. Higher output does not automatically mean tighter thickness control. Stable results depend on the coordination of extrusion, calendering, cooling, haul-off, and process control, as well as suitable equipment sizing and operation.
What information should be provided when selecting an SPC flooring extrusion line?
Provide the target sheet thickness and tolerance, sheet width, material formulation, planned production output, and downstream processing requirements. This information helps the supplier evaluate a suitable line configuration.